Machine control
Single stations, cells and complete production lines.
We speak the language of your automation systems. Our team programs across all major platforms — delivering solutions that just work, with no compatibility issues and no limitations.
Machine builders and plant engineering teams have the same constraint: the people who can write the control software are the same people who have to commission, support and improve the existing installed base.
We develop automation software offline for machines and production lines, so your internal team stays focused on commissioning and execution rather than being consumed by development.
Single stations, cells and complete production lines.
Vision, robots, motion, drives and enterprise systems.
Written and tested before shipment, validated on a digital twin.
Add engineers for a project peak without hiring overhead.
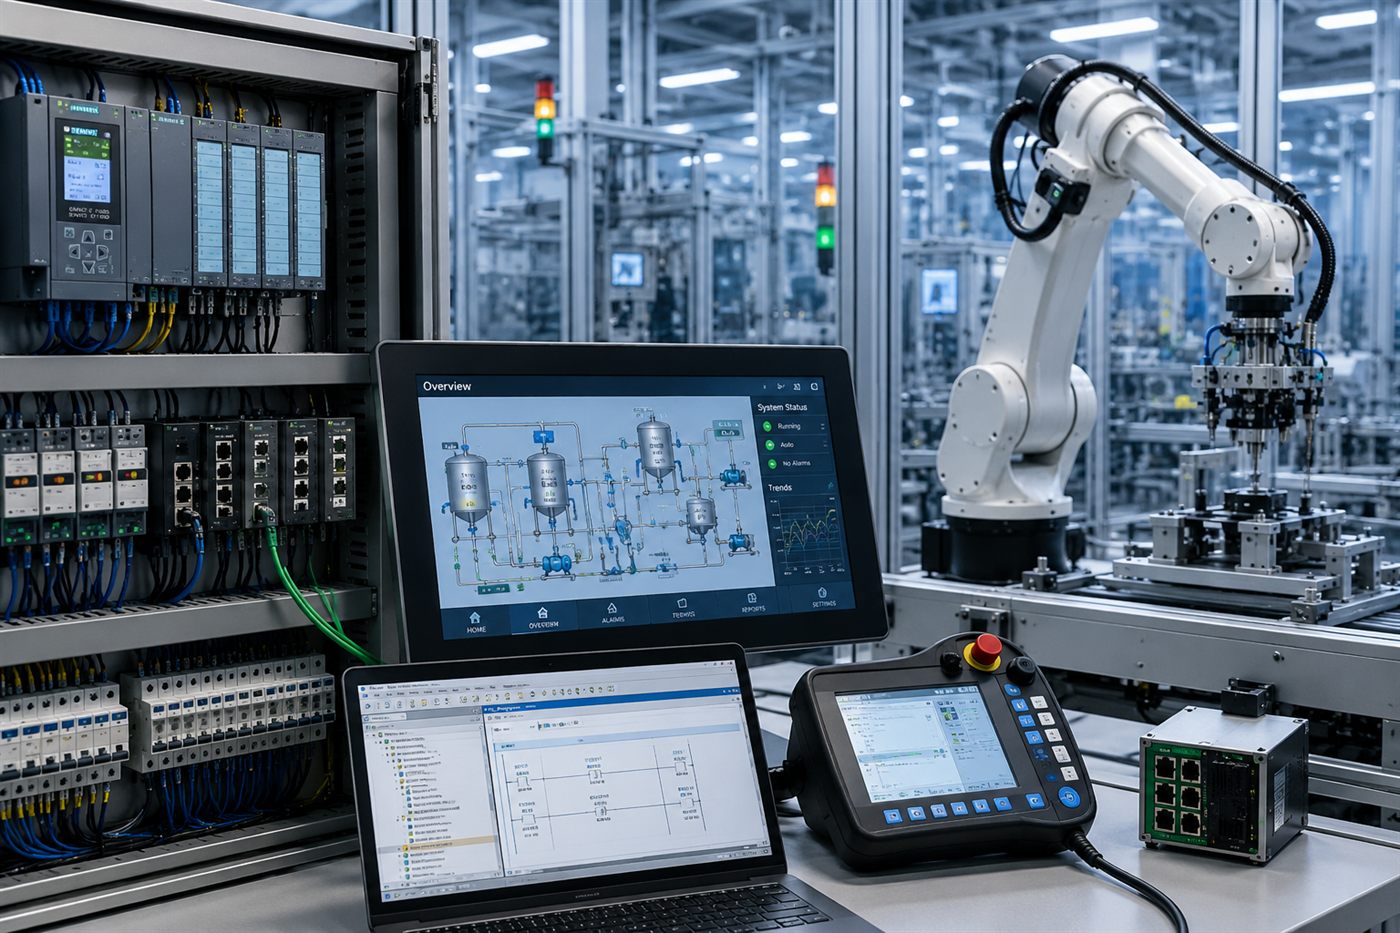
We work with the installed base you already have, rather than proposing a migration you did not ask for.
| Category | Platforms | Typical scope |
|---|---|---|
| PLC / PAC | Siemens S7-1200 & S7-1500 (TIA Portal), Rockwell / Allen-Bradley CompactLogix & ControlLogix, Beckhoff TwinCAT, Mitsubishi, Delta | Sequence logic, motion, interlocks, diagnostics |
| Robotics | KUKA, FANUC, ABB, Yaskawa | Path programming, TCP calibration, safety validation |
| HMI | WinCC, vendor-native panels across all supported brands | Operator screens, alarms, recipes, diagnostics |
| SCADA | Ignition Perspective & Vision, WinCC Professional | Plant visualisation, historian, OEE, reporting |
| Connectivity | OPC UA, MQTT, Modbus, PROFINET, EtherNet/IP | PLC-to-PC, MES and ERP integration |
We handle it all — and we document it well enough that someone else could maintain it.
Sequence-driven machine logic, recipe-driven batch operations and continuous process control within a single codebase convention.
Production counters, cycle timing, downtime capture and quality flags structured for MES consumption from day one.
Coordinated handshakes between controller, robot, vision system and servo axes — including offset correction and fault recovery paths.
Reliable, tested links to PC applications, databases, SCADA and MES over standard industrial protocols.
Advanced recipe handling, changeover management and order processing driven from ERP or MES.
Alarm strategy designed for operators rather than engineers, with historian and data logging built in.
Code is only part of it. The documentation is what makes the code an asset rather than a dependency.
Our standard: internal PLC & HMI programming guidelines aligned to IEC 61131-3 (languages) and IEC 81346-1 (structures), so the program reads the same regardless of which of our engineers wrote it.
Validate the exact code that will ship, against a simulated machine, before it leaves the office.
Service 08The engineers who wrote the code are the ones who debug it on your floor.
PlatformStructure the data your new program produces into automated OEE from the first shift.
Looking for something else?
Tell us the controller brand, the sequence and the cycle time. We will tell you how we would build it.
We value your privacy
This site stores a small amount of data on your device to remember your theme choice. If you accept, we will also measure how the site is used so we can improve it. Read our Privacy Policy.
We'll respond quickly within one business day!